Skip to content
Aluminum anodizing is one of the most widely used surface treatment processes for aluminum and aluminum alloys. The process uses electrochemical reactions to create a protective oxide layer on the surface of aluminum. This oxide layer significantly improves corrosion resistance, wear resistance, and surface durability. At the same time, the porous anodized layer can be colored using dyes or electrolytic coloring methods, making it possible to produce a wide range of decorative finishes.
Because of these advantages, anodized aluminum is commonly used in industries such as construction, electronics, automotive manufacturing, aerospace engineering, and consumer products. Modern anodizing technologies also allow manufacturers to produce a wide variety of anodized aluminum colors, giving designers more flexibility when developing products that require both durability and aesthetic appeal.
What Is Aluminum Anodizing?
Aluminum anodizing is an electrochemical process in which aluminum parts are placed in an electrolyte solution and connected to a power supply. During the process, the aluminum workpiece is connected as the anode, while another conductive material such as stainless steel or lead serves as the cathode. Many beginners often ask about anodized aluminum cathode or anode connections, but the principle is straightforward. The aluminum component must always act as the anode because oxidation occurs at the anode surface.
The main chemical reactions are:
Anode (aluminum part):
2Al + 3H₂O → Al₂O₃ + 6H⁺ + 6e⁻
Cathode (stainless steel or lead plate):
2H⁺ + 2e⁻ → H₂↑
To obtain a high-quality oxide layer, the process must carefully control voltage, current density, electrolyte concentration, and temperature.
When electric current passes through the electrolyte solution, oxygen ions react with the aluminum surface and form aluminum oxide. Natural oxide layers on aluminum are extremely thin and usually measure only 0.01 to 0.1 microns. Through anodizing, the oxide layer can grow to a thickness between 5 and 150 microns, greatly increasing the durability of the metal.
Another important characteristic of anodized aluminum is that the oxide layer is porous. These microscopic pores allow dyes or metallic salts to enter the surface, which makes aluminum coloring possible. After coloring, the pores are sealed to lock the color into the surface and improve corrosion resistance.
Why Aluminum Is Anodized
Manufacturers anodize aluminum primarily to improve durability, enhance appearance, and increase surface performance. Aluminum is naturally corrosion resistant, but the anodized oxide layer provides much stronger protection against moisture, chemicals, and environmental exposure. This makes anodized aluminum suitable for outdoor environments and industrial applications where long-term reliability is important.
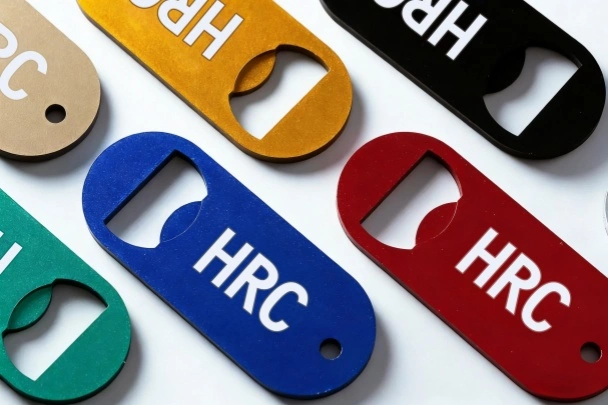
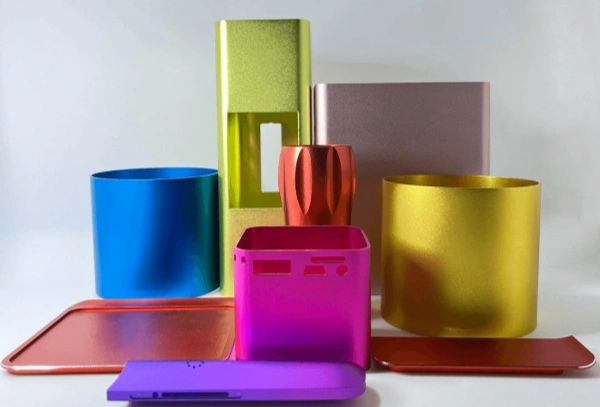
The decorative benefits of anodizing are also significant. Through dye coloring or electrolytic coloring, manufacturers can create a wide range of anodized aluminum colors, including black, bronze, champagne, blue, and gold.
In addition to protection and decoration, anodizing can improve mechanical performance. Hard anodizing processes can produce thicker oxide layers that increase hardness, wear resistance, and electrical insulation. Because of these advantages, anodized aluminum is often used in precision mechanical components and high-performance equipment.
Advantages and Limitations of Anodized Aluminum
Anodized aluminum offers several advantages compared with other surface treatment methods, such as painting, electroplating, or passivation. One of the most important benefits is that the oxide layer becomes part of the aluminum itself. Instead of sitting on the surface like paint, the anodized layer is integrated into the metal structure, which prevents peeling or flaking.
Another advantage is that anodizing does not apply a separate metal coating to the aluminum surface. Compared with some traditional plating processes, it can reduce reliance on certain heavy-metal coatings. However, proper chemical handling, wastewater treatment, and process control are still essential in industrial anodizing operations.
Despite these advantages, anodizing also has some limitations. Certain aluminum alloys with high copper content, such as 2024 or 7075, can produce darker or uneven oxide layers during anodizing. The anodized coating is also relatively brittle compared with the base metal, which means it may not perform well in parts that undergo heavy deformation. Dyed coatings may gradually fade under long-term exposure to strong ultraviolet light or extreme heat.
Preparation Before Anodizing
Preparation plays a critical role in determining the quality of anodized aluminum surfaces. Before anodizing begins, manufacturers must carefully select suitable aluminum alloys, prepare proper equipment, and ensure that the surface of the metal is clean and free of contaminants.
Different aluminum alloys respond differently during anodizing. Pure aluminum alloys such as 1050 and 1060 generally produce very uniform finishes and are commonly used for decorative applications. Alloys like 6061 and 6063 are widely used in industrial components and architectural structures because they balance strength and anodizing performance. Aluminum alloy 5052 is also frequently anodized due to its excellent corrosion resistance, which makes it suitable for marine or outdoor applications.
Surface preparation is also essential. Any machining marks, scratches, or contamination on the aluminum surface will remain visible after anodizing. For this reason, manufacturers often use polishing, brushing, or sandblasting before anodizing begins. Polishing produces smooth decorative surfaces, while brushing creates linear textures that are often used for architectural panels. Sandblasting produces matte finishes that are commonly used before colored anodizing.
The Aluminum Anodizing Process
Anodizing Process Principle
During anodizing, the aluminum part acts as the anode in an electrolytic bath. When direct current is applied, the aluminum surface reacts to form a controlled aluminum oxide layer.
As the oxide layer develops, a porous structure forms on the surface. These microscopic pores can absorb dyes or receive metallic deposits, allowing manufacturers to produce a wide range of anodized aluminum colors. After coloring, the pores are sealed to improve corrosion resistance and color retention.
The quality of the anodized finish depends on several process variables, including alloy composition, surface preparation, electrolyte concentration, temperature, current density, and treatment time.
Main Types of Anodizing
Aluminum anodizing is commonly classified into several types according to the electrolyte and required coating properties. The most widely recognized industrial processes include Type I, Type II, and Type III anodizing.
Type I – Chromic Acid Anodizing
Type I anodizing uses a chromic acid electrolyte to produce a relatively thin oxide coating. It is commonly associated with aerospace applications and components where corrosion resistance is required without significantly changing part dimensions.
Type II – Sulfuric Acid Anodizing
Type II sulfuric acid anodizing is one of the most widely used anodizing processes. It provides good corrosion resistance and can produce a variety of decorative finishes. Because the porous oxide layer readily accepts dyes, Type II anodizing is commonly used for black, blue, red, gold, and other colored aluminum parts.
Type III – Hard Anodizing
Type III, also known as hard anodizing or hardcoat anodizing, produces a thicker and harder oxide layer than conventional Type II anodizing. It is commonly used for components that require increased wear resistance, surface hardness, and durability.
Other anodizing processes, including oxalic acid anodizing, may also be used for specialized applications.
Industrial Aluminum Anodizing Process
Industrial anodizing requires careful process control to achieve consistent coating thickness, color, and surface quality. Although the exact procedure varies depending on the alloy, coating specification, and desired finish, a typical aluminum anodizing process includes the following steps:
1. Inspection and Surface Preparation
The aluminum parts are inspected for machining marks, scratches, contamination, and other surface defects. Depending on the required finish, the parts may also be polished, brushed, or sandblasted before anodizing.
2. Cleaning and Degreasing
Oil, grease, machining fluids, and other contaminants are removed from the surface. Proper cleaning is essential for achieving a uniform anodized finish.
3. Etching and Desmutting
Chemical etching may be used to create a more uniform matte surface, followed by desmutting to remove alloying residues and prepare the surface for anodizing.
4. Anodizing
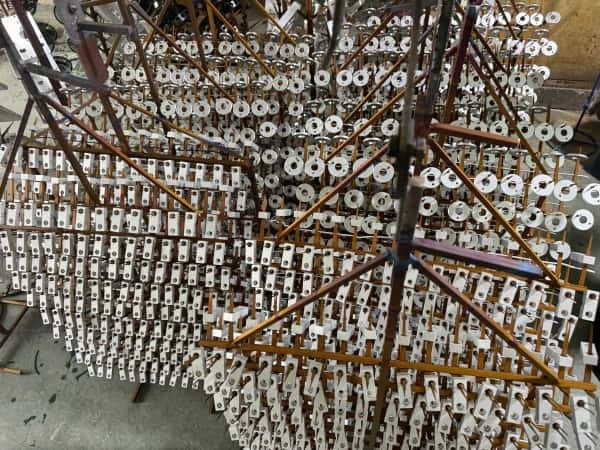
The aluminum parts are immersed in an electrolyte bath and connected as the anode. Controlled electrical current forms the aluminum oxide layer. Coating thickness and surface properties depend on factors such as electrolyte composition, temperature, current density, and processing time.
5. Rinsing
After anodizing, the parts are thoroughly rinsed to remove residual electrolyte before coloring or sealing.
6. Coloring
If a colored finish is required, dyes or electrolytic coloring methods can be used to produce the desired anodized aluminum color.
7. Sealing
The porous anodized layer is sealed to improve corrosion resistance, color retention, and long-term surface durability.
8. Final Inspection
Finished parts are inspected for coating thickness, surface appearance, color consistency, and other specified requirements before packaging and shipment.
Coloring Methods for Anodized Aluminum
One of the most appealing aspects of anodizing is the ability to create decorative colors on aluminum surfaces. Manufacturers typically use two primary methods to achieve these colors: dye coloring and electrolytic coloring.
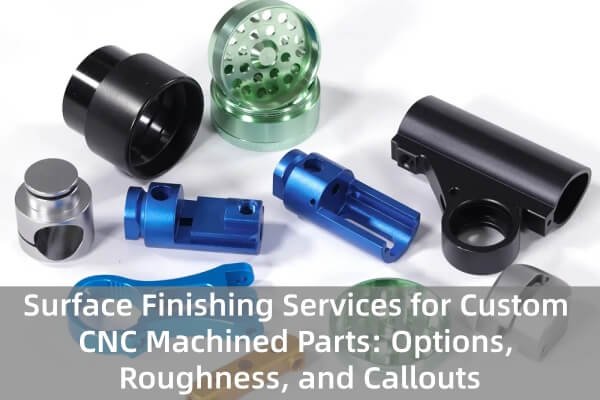
Dye coloring is the most common method used for aluminum coloring. After the anodizing process creates porous oxide layers, the aluminum parts are placed in dye baths. The dyes penetrate the pores and produce vibrant colors. Many consumer products use this technique to create finishes such as red anodized aluminum, blue anodized aluminum, or black anodized aluminum.
Electrolytic coloring is another method commonly used for anodized aluminum, particularly in architectural applications. Instead of organic dyes, this process deposits metallic compounds within the pores of the anodized layer. Careful control of the electrical conditions and process parameters is essential to achieve a uniform and consistent finish.
Electrolytic coloring typically produces more durable finishes than dye coloring, which is why it is widely used in building facades, window frames, and exterior architectural components.
Hard Anodizing and Advanced Anodizing Technologies
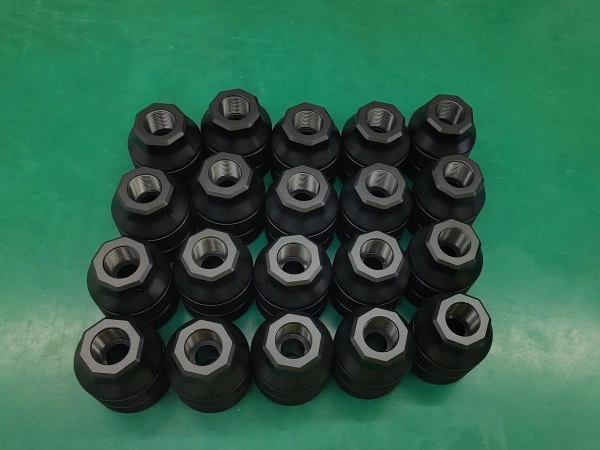
Hard anodizing is a specialized variation of the anodizing process designed to produce extremely durable oxide layers. In this process, lower temperatures and higher current densities are used to form thicker coatings that can range from 25 to 100 microns in thickness. Hard anodized surfaces are significantly harder than standard anodized coatings and provide excellent wear resistance.
Because of these properties, hard anodizing is commonly used for mechanical components such as machine parts, aerospace equipment, hydraulic systems, and automotive components. The hard anodized layer can withstand high friction and mechanical stress, which makes it valuable in demanding industrial environments.
Modern anodizing technology continues to evolve as manufacturers look for more environmentally friendly and efficient processes. New developments include chromium-free anodizing systems, pulse anodizing technologies, and automated production lines that improve consistency and productivity.
Applications of Anodized Aluminum
Anodized aluminum is widely used across many industries due to its durability, corrosion resistance, and decorative possibilities. In the construction industry, anodized aluminum is commonly used for curtain walls, window frames, and building facades. These architectural elements often require consistent surface finishes, which is why designers frequently rely on an anodized aluminum color chart when selecting specific finishes for large projects.
In the electronics industry, anodized aluminum is widely used for laptop housings, smartphone frames, and audio equipment enclosures. Many consumer electronics products feature decorative finishes such as red anodized aluminum or gold anodized aluminum to create distinctive visual designs.
Mechanical engineering applications also benefit from anodized aluminum. Hard anodized coatings improve wear resistance in components such as pistons, sliding mechanisms, and precision machine parts. In the automotive industry, anodized aluminum is used in performance components, decorative trim, and wheel parts because of its durability and corrosion resistance.
Consumer products also rely heavily on anodized aluminum. Furniture, lighting fixtures, cookware, and decorative items often feature anodized finishes that provide both visual appeal and long-term durability.
Cost Considerations in Aluminum Anodizing
The cost of anodizing aluminum depends on several factors, including part size, quantity, aluminum alloy, surface preparation, anodizing type, coating thickness, color requirements, masking requirements, and quality specifications.
Production volume can also significantly affect unit cost because multiple parts can often be processed in the same batch. For custom CNC machined parts, providing the drawing, material, quantity, required anodizing type, color, and critical surface requirements helps manufacturers prepare a more accurate quotation.
FAQ About Anodized Aluminum Colors
1. What colors can aluminum be anodized?
Aluminum can be anodized in a wide range of colors, including black, clear, blue, red, gold, bronze, green, and other custom shades. The available colors depend on the anodizing process, dye system, aluminum alloy, and surface finish.
2. Can anodized aluminum be matched to a specific color?
Yes, anodized aluminum can be produced to closely match a specified color sample or reference. However, exact color matching can be affected by the aluminum alloy, surface texture, coating thickness, dye concentration, and process conditions. For projects with strict appearance requirements, confirming an approved sample before production is recommended.
3. Why does anodized aluminum sometimes have color variations?
Color variation can result from differences in aluminum alloy composition, raw material batches, surface finish, anodized coating thickness, dye concentration, and sealing conditions. Maintaining consistent materials and tightly controlled process parameters helps minimize color differences between production batches.
4. Which aluminum alloys are best for color anodizing?
Aluminum alloys such as 6061, 6063, and 5052 are commonly used for anodizing and can produce attractive, consistent finishes when properly processed. However, different alloys respond differently to anodizing. Alloys with higher levels of copper, silicon, or other alloying elements may produce darker or less uniform colors.
5. How thick is an anodized aluminum coating?
Anodized coating thickness depends on the anodizing type and application requirements. Standard decorative anodizing typically produces a thinner coating, while Type III hard anodizing creates a thicker coating for improved wear resistance and durability. The required thickness should be specified according to the part’s functional and dimensional requirements.
6. Does anodizing affect part dimensions and tolerances?
Yes. Anodizing creates an oxide layer on the aluminum surface, so coating thickness must be considered when designing precision CNC machined parts. For tight-tolerance features, threaded areas, mating surfaces, or critical dimensions, anodizing requirements should be defined before machining so appropriate allowances or masking can be planned.
7. How long does the color on anodized aluminum last?
A properly anodized and sealed aluminum finish can maintain its appearance for many years. Color durability depends on the coloring method, sealing quality, UV exposure, temperature, chemicals, and operating environment. For outdoor or high-UV applications, the coloring method should be selected according to the expected service conditions.
8. Can Aluminum Be Anodized Blue?
Yes. Blue anodized aluminum is typically produced by adding a suitable dye after the anodizing process and before sealing. The final shade can vary depending on the aluminum alloy, surface finish, coating thickness, and dyeing conditions.
Need CNC machined aluminum parts with a consistent anodized finish?
HRCCNC provides CNC machining and anodizing support for custom aluminum components, from prototypes to production runs. Send us your CAD files or drawings along with your alloy, color, surface finish, coating, and tolerance requirements. Our team can review your project and help determine a suitable machining and anodizing solution before production.
Contact HRCCNC to request a quote for your custom anodized aluminum parts.